Softness starts with space.
Spring starts with structure.
Space to move.
Structure to return.
Load the cells. Watch the walls move. Release the load. Watch the network recover.1
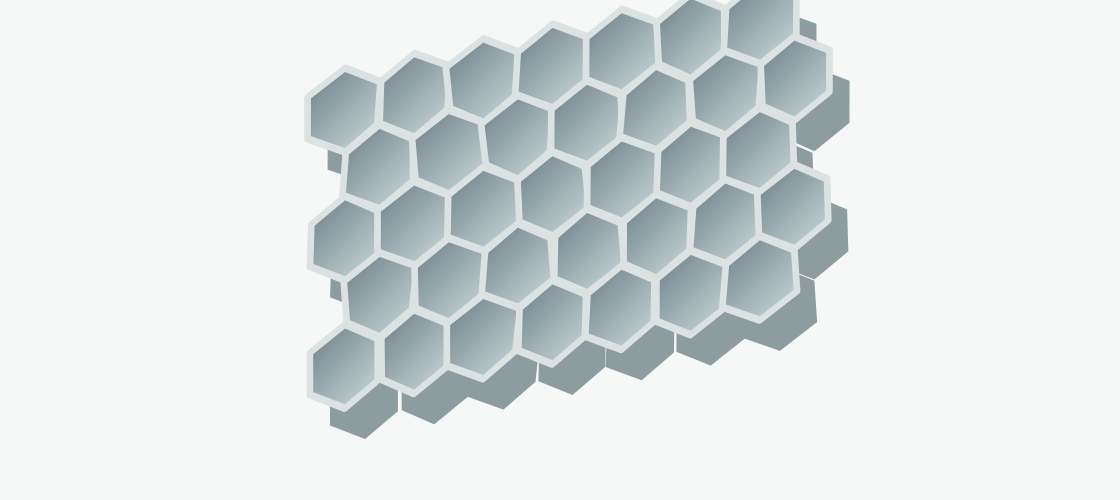
The solid networkWalls carry load and change shape.
The cellular spaceVoids make room for deformation.
UnloadedA structure ready to compress.
Walls and gas-filled cells form a structure that can deform under load and recover as the load is removed.
A familiar feeling.
A closer look.
Five balls help picture the engineering. Choose a foam. Squeeze, release, look inside.
A foam practice ball.
Air spaces make room to compress.
Space within a connected network.
Ball types are analogies, not foam ratings. A-TPU is part of the TPU family.
EVA · A foam practice ball.
Many small cells. Room to squeeze.
In many EVA foams, permanent links join polymer chains. The network deforms as the cells compress.
TPU · A basketball.
Give and support, working together.
In TPU, harder regions help hold flexible chains together. The foam has many cells, unlike the ball’s single air chamber.
A-TPU · A volleyball.
A familiar construction. A different recipe.
A-TPU changes the isocyanate used to make TPU. It keeps the flexible-segment and hard-region architecture.
PEBA · A rubber bouncy ball.
The material moves. Then moves back.
PEBA joins flexible polyether segments to harder polyamide regions. Their chemistry and proportions can be tuned.
TPEE · Inside a baseball.
Different parts. Different jobs.
TPEE pairs flexible segments with crystalline polyester regions. These are molecular regions, not a ball’s literal layers.
The chemistry, in more detail
EVA · Ethylene–vinyl acetate
The acetate groups interrupt a pattern. EVA has a statistical chain architecture. It should not be pictured as long alternating hard and soft blocks. Increasing vinyl-acetate content changed crystal formation and melting in a study of three resin grades. The study establishes a useful chemical control, without defining every footwear formulation. Read the resin study.
The covalent crosslinks used in many EVA foams serve a different purpose from the acetate groups. They connect chains into a network. Calling those connections an inherent defect misses their engineering role: the network helps resist flow while bubbles grow. A material can have permanent chemical connections and still undergo recoverable deformation.
A laboratory comparison makes the process distinction tangible. Researchers used peroxide-crosslinked EVA with either a decomposing blowing agent or pressurized nitrogen. The physically blown samples had a different cellular morphology. Nitrogen changed how gas entered and expanded; it did not remove the previously formed network. Read the foaming comparison.
For a runner, the useful consequence is to keep the recipe open. The word EVA does not reveal the blend, filler content, degree of expansion or thickness under the heel. Comparing two differently shaped shoes cannot isolate the effect of their blowing process, even if their labels emphasize that difference.
Ask what was measured next. A foam coupon, a complete shoe and a person running answer different questions. A rebound result describes recovery in one test; repeated loading asks how that response changes. Neither supplies a universal retirement distance. The molecular sketch is a way to understand the design choices, not a verdict on every shoe containing EVA.
TPU · Thermoplastic polyurethane
There are two kinds of connection to keep apart. Hard and soft segments are covalently connected along a TPU chain. Hard segments on different chains can then associate into hard-rich domains. These physical junctions are not the same thing as permanent bridges between chains. Heating changes their organization enough to permit thermoplastic processing. Explore the architecture.
The diagram is deliberately simplified. Real material can include mixed regions rather than two perfectly separated populations. Hard-segment chemistry, soft-segment chemistry and their proportions give manufacturers several controls. A picture of flexible strands connected by identical blocks cannot specify a resin’s actual response.
Processing adds another set of choices. BASF’s current portfolio includes aromatic TPU for supercritical injection as well as expanded-bead applications. It also includes aliphatic TPU in several routes. A bead-shaped surface therefore identifies an assembly strategy, while the TPU label identifies a much broader chemical family. See the supplier’s routes.
This matters when comparing shoes across generations. If a newer midsole is lighter, the label alone cannot tell us how much came from resin selection, expansion, part dimensions or the rest of the shoe. Those are separate explanations that need separate evidence. A chemical category cannot substitute for a mass measurement.
Read a rebound number with the same care. Specify whether it came from an impact device, a compression cycle or bending the complete shoe. Then ask about load, speed, temperature and prior cycling. Physical junctions explain an important route to elasticity; they do not promise that all deformation disappears or that a given fraction of mechanical work becomes a metabolic saving for the runner.
A-TPU · Aliphatic thermoplastic polyurethane
The A describes a chemical choice, not another category of foam production. Aliphatic TPU remains TPU. Its isocyanate building block differs from that of aromatic TPU, while the material still combines hard and soft segments. Some aliphatic choices are linear; cycloaliphatic choices contain saturated rings. There is no single molecular shape hiding behind the abbreviation.
A controlled polyurethane study illustrates why a simple story can fail. Researchers compared several isocyanates while retaining the same polyol and chain extender. The HDI-based material showed the highest crystallinity and hardness in their series. Greater flexibility of one building block did not produce a universally softer finished polymer. This was a nonfoam experiment, not a racing-shoe comparison. Read the structure study.
The manufacturing choices are also plural. BASF lists aliphatic grades for bead molding, autoclave processing and SCF injection. Its grade specifications are useful examples of achievable combinations. They should remain attached to their stated test, rather than becoming a family-wide performance range. See the grade portfolio.
For a runner, this leaves a concrete distinction between possibility and proof. Chemistry can enable a designer to pursue a particular midsole. Establishing what that midsole achieves requires measurements on the resulting product. Even two shoes using aliphatic TPU need not have matched formulations, density, dimensions or loading conditions.
Durability deserves the same scrutiny as first impressions. Ask which property was retained, after what kind of loading, and whether specimens were allowed to recover before testing. A laboratory cycle count and road distance are different exposures. Until those comparisons are available, “aliphatic” should help explain the material choice without becoming a promise about the runner’s next several hundred kilometers.
PEBA · Polyether block amide
PEBA puts two useful kinds of block on the same chain. The polyamide and polyether portions give the material distinct structural roles. Their relative amounts and chemistry are design choices. Arkema’s Pebax family includes PA12-based grades and a PA11-based Rnew range, so even a familiar trade name does not identify one molecular recipe. Explore the block family.
The next structure appears when the resin is foamed. Gas uptake, crystal formation and cell growth interact. Researchers studying PEBA deliberately changed crystallization conditions before CO₂ foaming and obtained both uniform and bimodal cell structures. Crystals provided sites for heterogeneous nucleation. The process did not create an identical population of bubbles merely because the gas was supercritical. Read the cell-structure study.
That distinction keeps a molecular diagram from doing too much work. It shows why PEBA offers an adjustable architecture; it cannot calculate the response of an unseen shoe. To make that calculation meaningful, we would also need information about the foam, the part dimensions, the boundary conditions and the load.
A return percentage needs an input quantity as well. Returning a large fraction of a small amount of mechanical work is different from returning the same fraction of a larger amount. A complete-shoe test can measure compression and recovered work together. A human running experiment must then establish whether the complete design changes metabolic cost.
The same restraint applies over time and temperature. Initial response, response after repeated loading and response after recovery are separate observations. Calling a material highly elastic does not settle all three. PEBA is a valuable piece of the explanation, but a runner buys the particular shoe in which its chemistry, cellular structure and geometry have been combined.
TPEE · Thermoplastic polyester elastomer
Polyester names one important part of the architecture. In the PBT/PTMG system studied here, the hard blocks are polyester and the soft blocks are polyether. This combination belongs to the broader family of thermoplastic polyester elastomers. The diagram represents that common architecture rather than every possible commercial grade.
Jiang and colleagues varied the block ratio and investigated CO₂ foaming. The changes affected crystallinity, melting behavior and the processing conditions. Gas also interacted differently with the soft and hard segments. These observations connect molecular organization to manufacturing: a processor needs a workable combination of gas uptake, expansion and structural support. Read the primary foaming study.
None of those observations gives a complete running sensation. A material experiment can identify a useful control without identifying the best setting for every shoe. Describing a polymer as stiff also leaves a question open: are we discussing the unfoamed resin, the cellular material, or the assembled part? Those are different objects.
Imagine receiving two midsoles labeled TPEE with no other information. The label would not tell you whether their masses match, whether their thicknesses match or whether their heel and forefoot structures match. A fair comparison would record those quantities and then specify how force was applied. The experiment would be comparing the actual designs rather than filling in their behavior from a category.
This is especially important for claims about lateral stability or durability. Neither follows directly from a hard-block sketch. Those questions require appropriate loading directions, repeated use and measurements of the outcome being claimed. TPEE adds another set of chemical and manufacturing options to the designer’s toolkit. The runner’s evidence still begins with the finished foam and continues through the complete shoe.
The gas is the tool.
The cells are the result.
1Dissolve the gas
Pressure helps CO₂ or nitrogen enter the polymer.
2Grow the cells
Changing conditions lets bubbles form and grow.
3Keep the structure
The process stabilizes the new cellular structure.
Physical foaming uses a gas such as CO₂ or N₂. Pressure, temperature, gas uptake and polymer structure work together; “supercritical” is a processing condition, not a new polymer.
What the factory can change
From dissolved gas to a cellular solid
In physical foaming, gas dissolves in the polymer under controlled conditions. Changing those conditions can create supersaturation: gas collects into nuclei, which grow into cells. Gas diffusion, viscosity, crystallization and the material’s resistance to stretching compete during that growth. Pressure alone is not a recipe.
Supercritical CO₂ and nitrogen are useful processing fluids. The polymer backbone does not become a new chemistry, but the process can change crystallinity, morphology and the properties of the finished foam. A physically foamed EVA can still have a covalently crosslinked network.611
Two different scales in bead foam
An expanded bead already contains cells. Joining many beads creates a second scale: the interfaces between them. In the steam-chest route described by BASF, steam heats and softens the bead surfaces so they join. It should not be confused with the gas used for the earlier expansion. A poorly joined interface and a damaged cell wall are different failure locations.2
A process name is not a performance specification
BASF lists aliphatic TPU across steam-chest, autoclave and supercritical-injection processing. That is a useful counterexample to the idea that TPU always means visible beads or that A-TPU always means a milled block. Polymer, expansion, joining and final shaping are separate choices.8
Softness. Spring.
Different jobs.
Squeeze measures movement. Rebound reveals returned energy.3
Same force. Different compression.
Illustrative specimens, not material ratings. A ball’s rebound height is a test-specific measure; running economy requires a runner.
Why test methods change the answer
In an instrumented compression test, mechanical work is the area under a force–displacement curve. The loading area records work put into the system; the unloading area records work returned. Their difference is the loop loss. In a settled cycle returning to the same state, this loss is dissipated. Initial cycles can involve residual deformation and delayed recovery; missing mechanical work is not a direct heat measurement. A resilience percentage describes that particular loading cycle and specimen.
A ball-rebound or pendulum test imposes a different event and reports a different test metric. Compression of a material sample, compression of a complete shoe, and three-point bending of a shoe should not share an unlabeled percentage chart. Each measures a different system or deformation.
Under a common force target, a more compliant shoe can deform farther and take in more work. It may therefore return more joules both because its returned fraction is higher and because more work entered it. Shorten’s methodological analysis is a useful reminder to report the denominator, test control, units and object—not only the headline percentage.313
The numbers need
a pair of shoes.
Now measure a whole shoe. Keep the test attached to the number.
A percentage is only half the story.
Returned work depends on how much enters the shoe, and how much comes back.
Whole shoes, not isolated polymers. Construction differs across models. Mechanical return is not a running-economy improvement. Hoogkamer et al., Figure 3 ↗
Exact values & study conditions
A rigid foot-form applied approximately 2,000 N over a 185 ms contact period. The prototype combined PEBA, a carbon plate and a different geometry. This protocol cannot isolate polymer chemistry.
| Shoe | Construction | Compression (mm) | Returned work (J) | Return (%) |
|---|---|---|---|---|
| Nike Zoom Streak 6 | EVA + rearfoot airbag | 6.1 | 3.28 | 65.5 |
| adidas Adios Boost 2 | TPU midsole | 5.9 | 3.56 | 75.9 |
| Nike prototype | PEBA + carbon plate | 11.9 | 7.46 | 87.0 |
Figure 3 values; uncertainty is not shown. The Streak’s 3.28 J figure label differs from 3.38 J in the discussion prose.
Wear changed these two shoes differently.
After 450 km, metabolic cost rose significantly in the PEBA prototype. The EVA prototype’s change was not significant.
Two prototypes. Two measured wear states. Twenty-two trained men tested the shoes at 13 km/h. This does not establish either polymer’s service life. Rodrigo-Carranza et al., Table 2 ↗
Exact values & study conditions
One researcher accumulated 450 km on asphalt over 40 sessions, at approximately 13 km/h. The laboratory crossover used four-minute trials at 20–23°C with 22 trained men. Both prototypes had carbon plates, but their dimensions differed. Segments connect measured means; no intermediate distances were tested.
| Prototype | Fresh | After 450 km |
|---|---|---|
| EVA prototype | 15.15 ± 1.13 | 15.13 ± 1.14 |
| PEBA prototype | 14.87 ± 0.99 | 15.21 ± 1.01 |
SD describes variation among the 22 participants, not uncertainty of the paired change. These metabolic results are separate from the paper’s mechanical bending tests.
What changes with time, temperature and use?
Wear is a history, not a polymer label. Repeated loading can change cell geometry, wall integrity and bulk mechanical properties. Material composition, density, processing, temperature and the loading history all matter. Aimar and colleagues combined mechanical testing with micro-CT to examine fatigue in specific commercial EVA, TPU and PEBA foams. Those specimens do not establish a universal lifetime for each family.1
Temperature changes the test. Meuchelböck and colleagues measured temperature-dependent compression behavior in a specific expanded-TPU grade. That supports asking how a particular material changes in the cold. It does not support assigning every EVA the same freezing behavior, or claiming that every PEBA and A-TPU shoe is temperature-invariant.4
Separate bending from compression. The 450 km study includes three-point bending measurements. Those mechanical return values cannot be relabeled as vertical foam-compression efficiency. Its running-economy results are measurements of people running in those complete shoe constructions.14
Bring better questions
to your next run.
Three questions to take into your next pair.
Room to compress.
How far does the finished shoe move under load?
Less lost in the cycle.
Was the foam tested, the shoe tested, or a person running?
A ride that lasts.
What changed after use—and what was measured?
Learn the molecule.
Look at the cells.
Judge the whole shoe.
These are interpretation questions, not a prescription or a ranking of individual shoes. Fit, task and the finished construction remain part of the decision.
Go deeper.
The research approach & what remains unknown
This issue is a source-based materials explainer, not a systematic review or a new experiment. Peer-reviewed studies support the experimental results; technical material from polymer suppliers supports attributed descriptions of architecture and manufacturing. Supplier specifications are not treated as independent whole-shoe or running-economy measurements.
We began with two supplied drafts and audited their claims against primary sources. Broad family rankings, unqualified lifetimes, mixed-method return tables and proprietary recipes without a verifiable source were removed or narrowed. The originals are retained unchanged in the working research packet.
Most proprietary grades, blend ratios, cell distributions and factory cycles are not fully public. A foam trade name can persist across different formulations. This issue deliberately avoids assigning undisclosed recipes or promising an individual runner an efficiency gain.
Read the complete research essay · Open the claim and correction ledger
Sources, methods & access notes
- Aimar et al. (2024). Compression fatigue of elastomeric foams used in midsoles of running shoes.Primary research; full text, Tables 1–2 and Figures 2–5 inspected. Extracted commercial foam specimens, 200,000 compression cycles. Specific formulations, densities and geometries; no universal mileage conversion. Two authors affiliated with Decathlon.
- BASF. Small beads for long distances.Manufacturer process description: expanded TPU particles are subsequently fused using heat/steam. Explains the route, not comparative running performance.
- Shorten (2024). Energy return in footwear – revisited.Methodological paper. Publisher abstract and indexed publisher excerpts inspected; direct full-text access returned 403. No numerical chart is taken from this source. Definitions are also supported by the compression study methods.
- Meuchelböck et al. (2024). Influence of temperature on the compression properties of expanded thermoplastic polyurethane (ETPU).Primary research; full methods/results consulted. Named Infinergy grade, foam specimens, controlled density/temperature and quasi-static compression. Does not establish a family-wide ranking or a running-rate temperature response.
- EVA: changing the vinyl-acetate contentShi et al., 2008. Primary paper; full-text methods, crystallization results and conclusions consulted. Unfoamed resin grades, not finished shoes.
- EVA: chemical and physical foaming comparedLi et al., 2024. Primary paper; full-text methods and morphology results consulted via an open-access PDF. Specific crosslinked EVA formulations.
- TPU: how hard and soft segments organizeCovestro technical explainer. Manufacturer text consulted; useful for architecture and processing, not an independent performance comparison.
- TPU: one family, several manufacturing routesBASF Infinergy portfolio, checked September 2026. Manufacturer specifications for named grades; listed pendulum rebound is not whole-shoe compression return.
- Isocyanate structure changes polyurethane propertiesWang et al., 2024. Primary nonfoam polyurethane experiment. Abstract and indexed results/conclusion passages consulted; full article not retrieved end to end.
- PEBA: polyamide blocks and polyether blocksArkema Pebax technical product page. Manufacturer description of polymer architecture and grade variation, not a finished-shoe test.
- PEBA: crystals change cell formationWang et al., 2023; DOI 10.1016/j.supflu.2023.106030. Primary study; abstract and publisher preview consulted. Controlled laboratory foaming, not commercial shoe recipes.
- TPEE: block ratio changes the foaming processJiang et al., 2020. Primary study; English and Chinese abstracts plus figure captions consulted. PBT/PTMG grades; no human running experiment.
- Hoogkamer et al. (2018) — A Comparison of the Energetic Cost of Running in Marathon Racing ShoesFull methods and results read. Mechanical observations: §2.2 and Figure 3. The chart follows Figure 3’s 3.28 J for the Streak; discussion prose prints 3.38 J. Whole-shoe construction differs across models. Study funded by Nike, with company employees and a consultant among the authors.
- Rodrigo-Carranza et al. (2024; online 2023) — Influence of different midsole foam in advanced footwear technology use on running economy and biomechanics in trained runnersFull methods and results read. Metabolic data: Table 2; wear protocol: §2.2. The separate Table 1 mechanical-return measurements concern whole-shoe bending, not vertical foam compression. Prototypes supplied by On; one author disclosed research grants from Puma and Saucony.
- ITF (2026). Technical booklet — foam training balls.§1.1. Governing-body technical text distinguishes foam training balls from hollow rubber-core tennis balls. Supports the ball analogy only.
- Molten (2017). Basketball and volleyball construction.Printed pp. 10–12 and 32. Manufacturer describes cover, winding and bladder. These macroscopic layers are not molecular domains in TPU.
- Cross (1999). The bounce of a ball.§§IV–V, Figures 2 and 5. Primary impact/compression experiments. Ball behavior is a teaching example, not a ranking of midsole polymers.
- Rawlings R100-H2 — baseball construction.Manufacturer description: cushioned-cork center, wool winding and leather cover. Used only for a parts-have-different-jobs analogy; not a claim about TPEE hardness.
Graphics & credits
Article, diagrams and procedural cellular artwork: YEAH. The cellular and molecular graphics are original conceptual illustrations. They are not microscopy, measured deformation, a proprietary formulation or product CAD. Evidence charts redraw the reported values and identify the original studies.
Three.js r180, used for the optional 3D renderer, is distributed under its MIT license. All typography uses system fonts. No documentary photographs or third-party product films are used in this issue.
Reading references supplied by the user: Running Warehouse’s foam guide and Sagasu Running’s “Running Shoe Foams Explained”. The retailer article was read; video metadata and description were inspected, but a transcript was unavailable. Neither is used as the authority for quantitative charts.